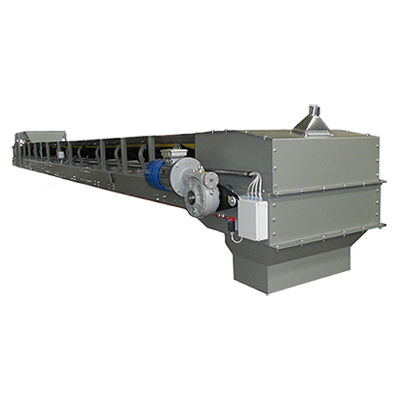
Bulk Material Conveyor
Bulk material conveyors are designed for the safe transportation of granular, powdered, and fine materials, offering high conveying capacity, an enclosed structure, and effective dust containment.
Product Details
Bulk material conveyors are designed for the safe transportation of granular, powdered, and fine materials, offering high conveying capacity, an enclosed structure, and effective dust containment. They can be used to transfer products such as detergent powder, coal dust, boron minerals, and similar bulk materials between production processes.
Special scrapers, brush systems, sealed inspection covers, and maintenance access points are used to minimize material loss and prevent dust from escaping into the surrounding environment. An automatic belt-tracking mechanism helps prevent belt misalignment and supports safe, stable conveyor operation.
Belt switches and monitoring systems continuously check the operating condition of the conveyor belt. When inspection or maintenance covers are opened, magnetic sensors transmit a signal to the safety system, helping protect personnel and equipment.
Depending on the application, the conveyor can be manufactured with hygienic, heat-resistant, impact-resistant, and heavy-duty belt, frame, and equipment options.