Motion Up Elevator
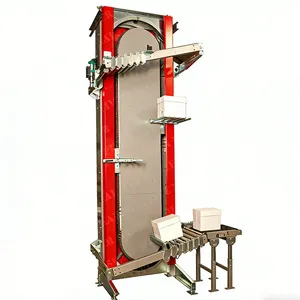
The Motion Up Elevator is designed for the automatic, fast, and safe transportation of products between different floors and elevation levels.
Product Details
The Motion Up Elevator is designed for the automatic, fast, and safe transportation of products between different floors and elevation levels. It is particularly suitable for multi-storey facilities with high production capacities, ensuring continuous product transfer.
Operating on a conveyor-based principle, the system can achieve transportation speeds up to five or six times faster than conventional elevators. It enables safe product movement between mezzanine warehouses and production floors without requiring personnel to enter the elevator area.
Thanks to its modular design, multiple units can be installed side by side or in different sections of the facility. This provides a flexible and highly efficient vertical conveying solution tailored to the plant layout and production capacity.