Our quality and reliable product portfolio
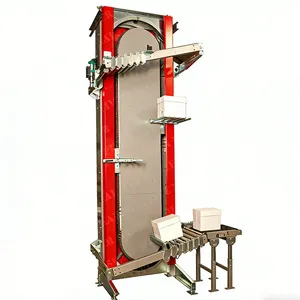
The system consists of two parallel flexible conveyors designed to move products vertically upward or downward.
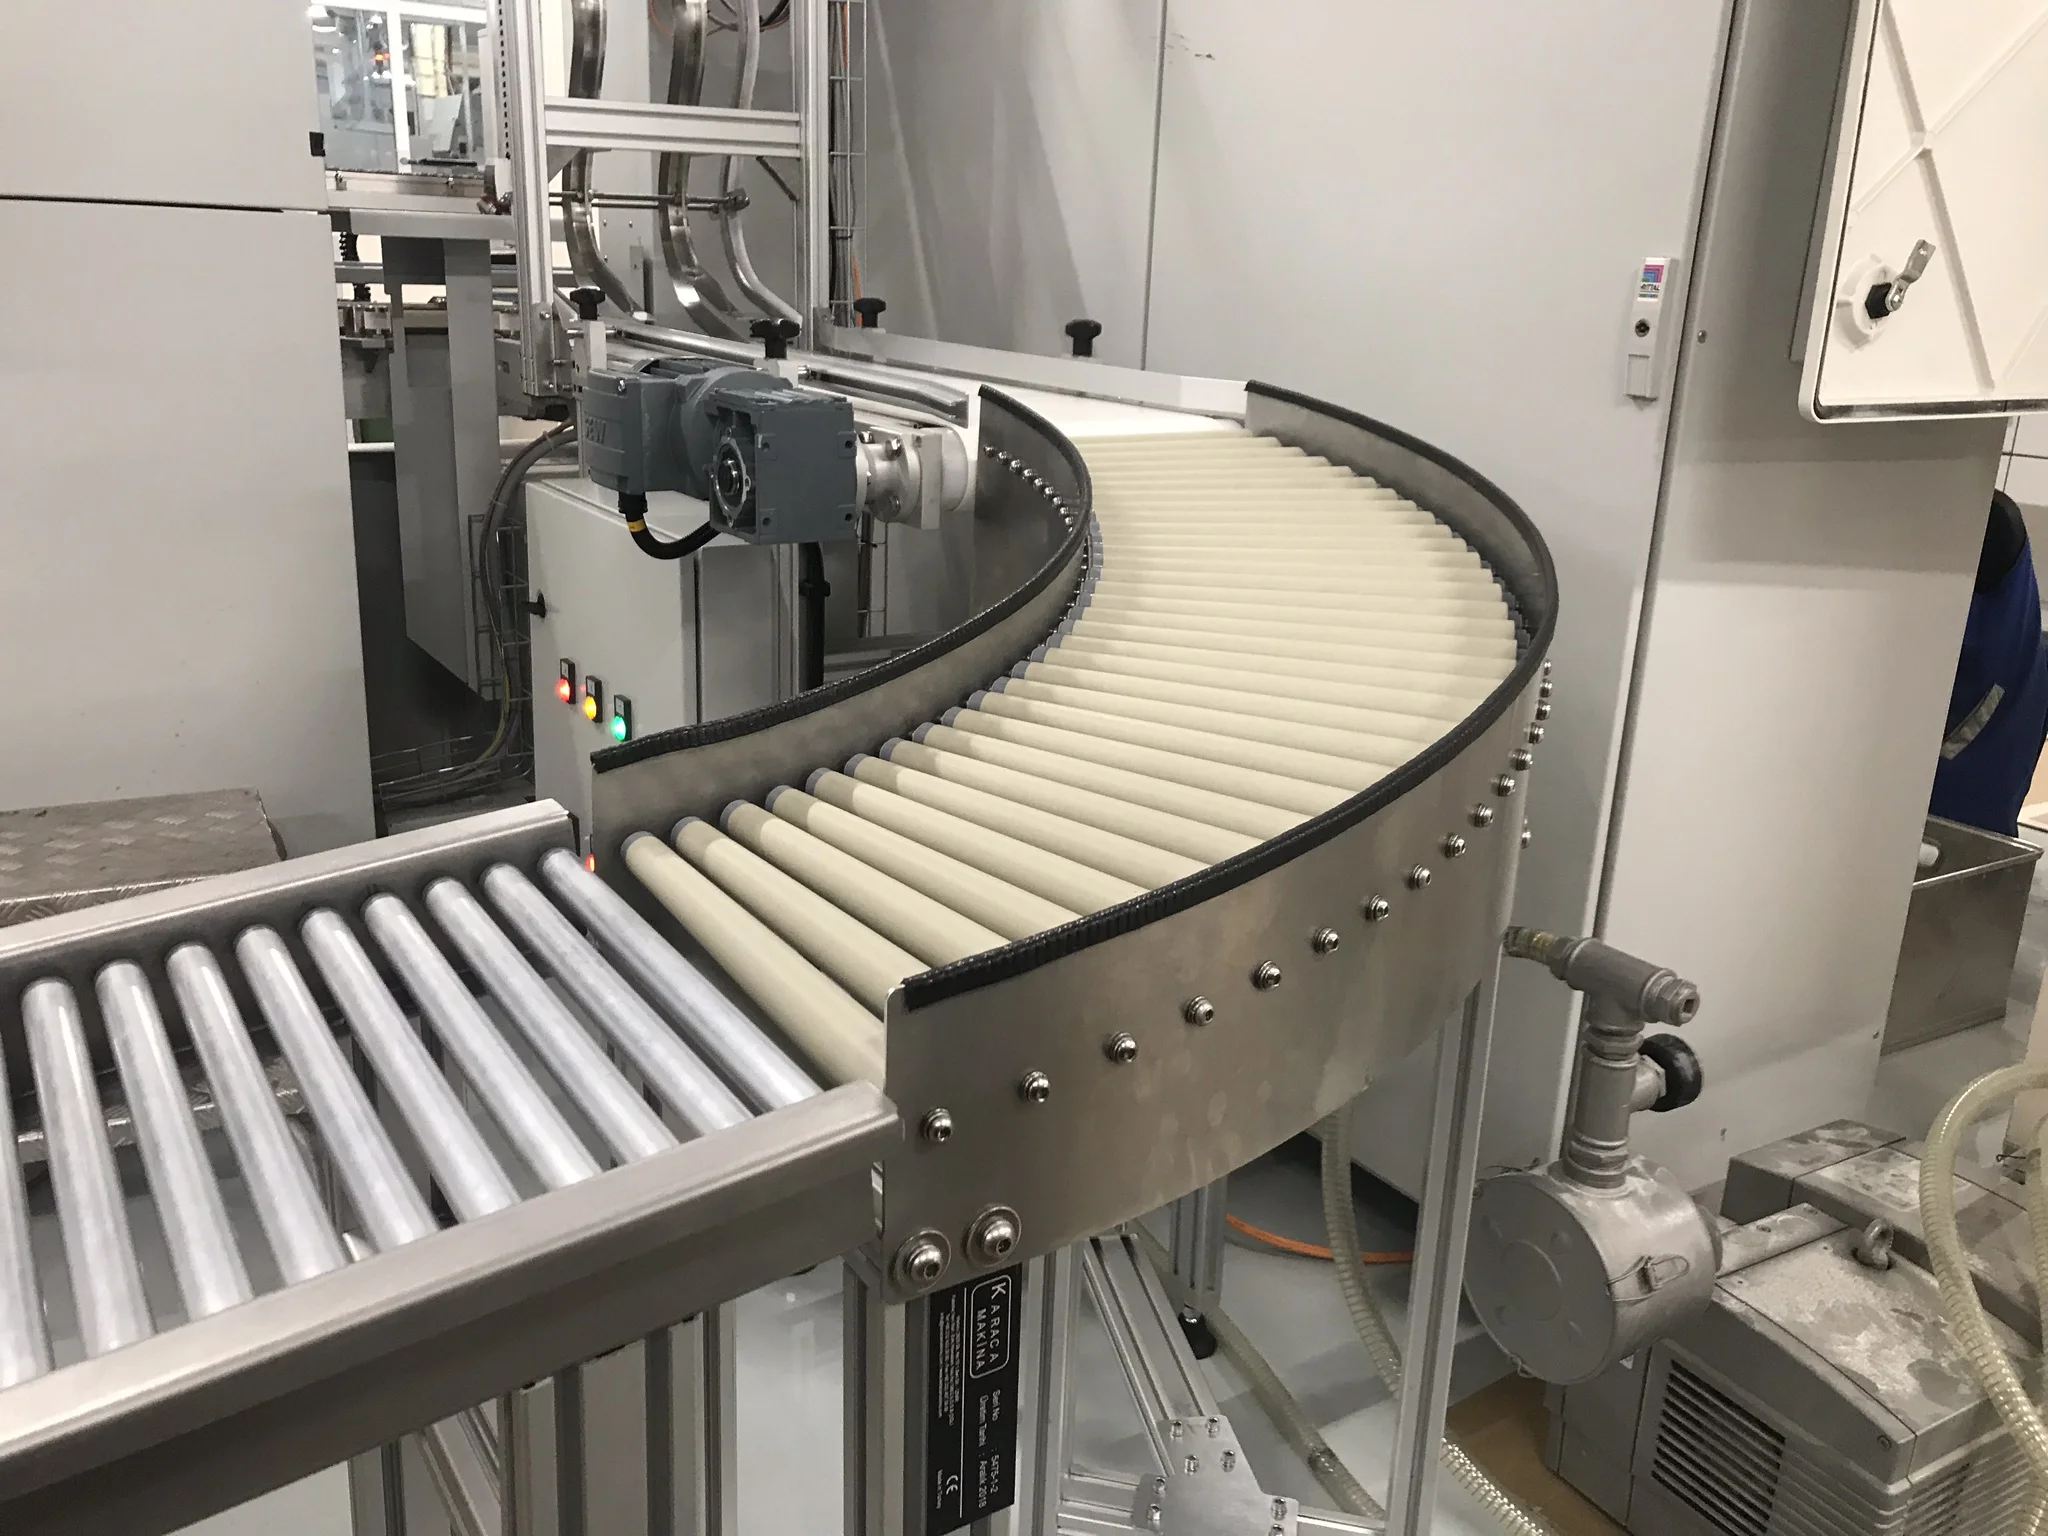
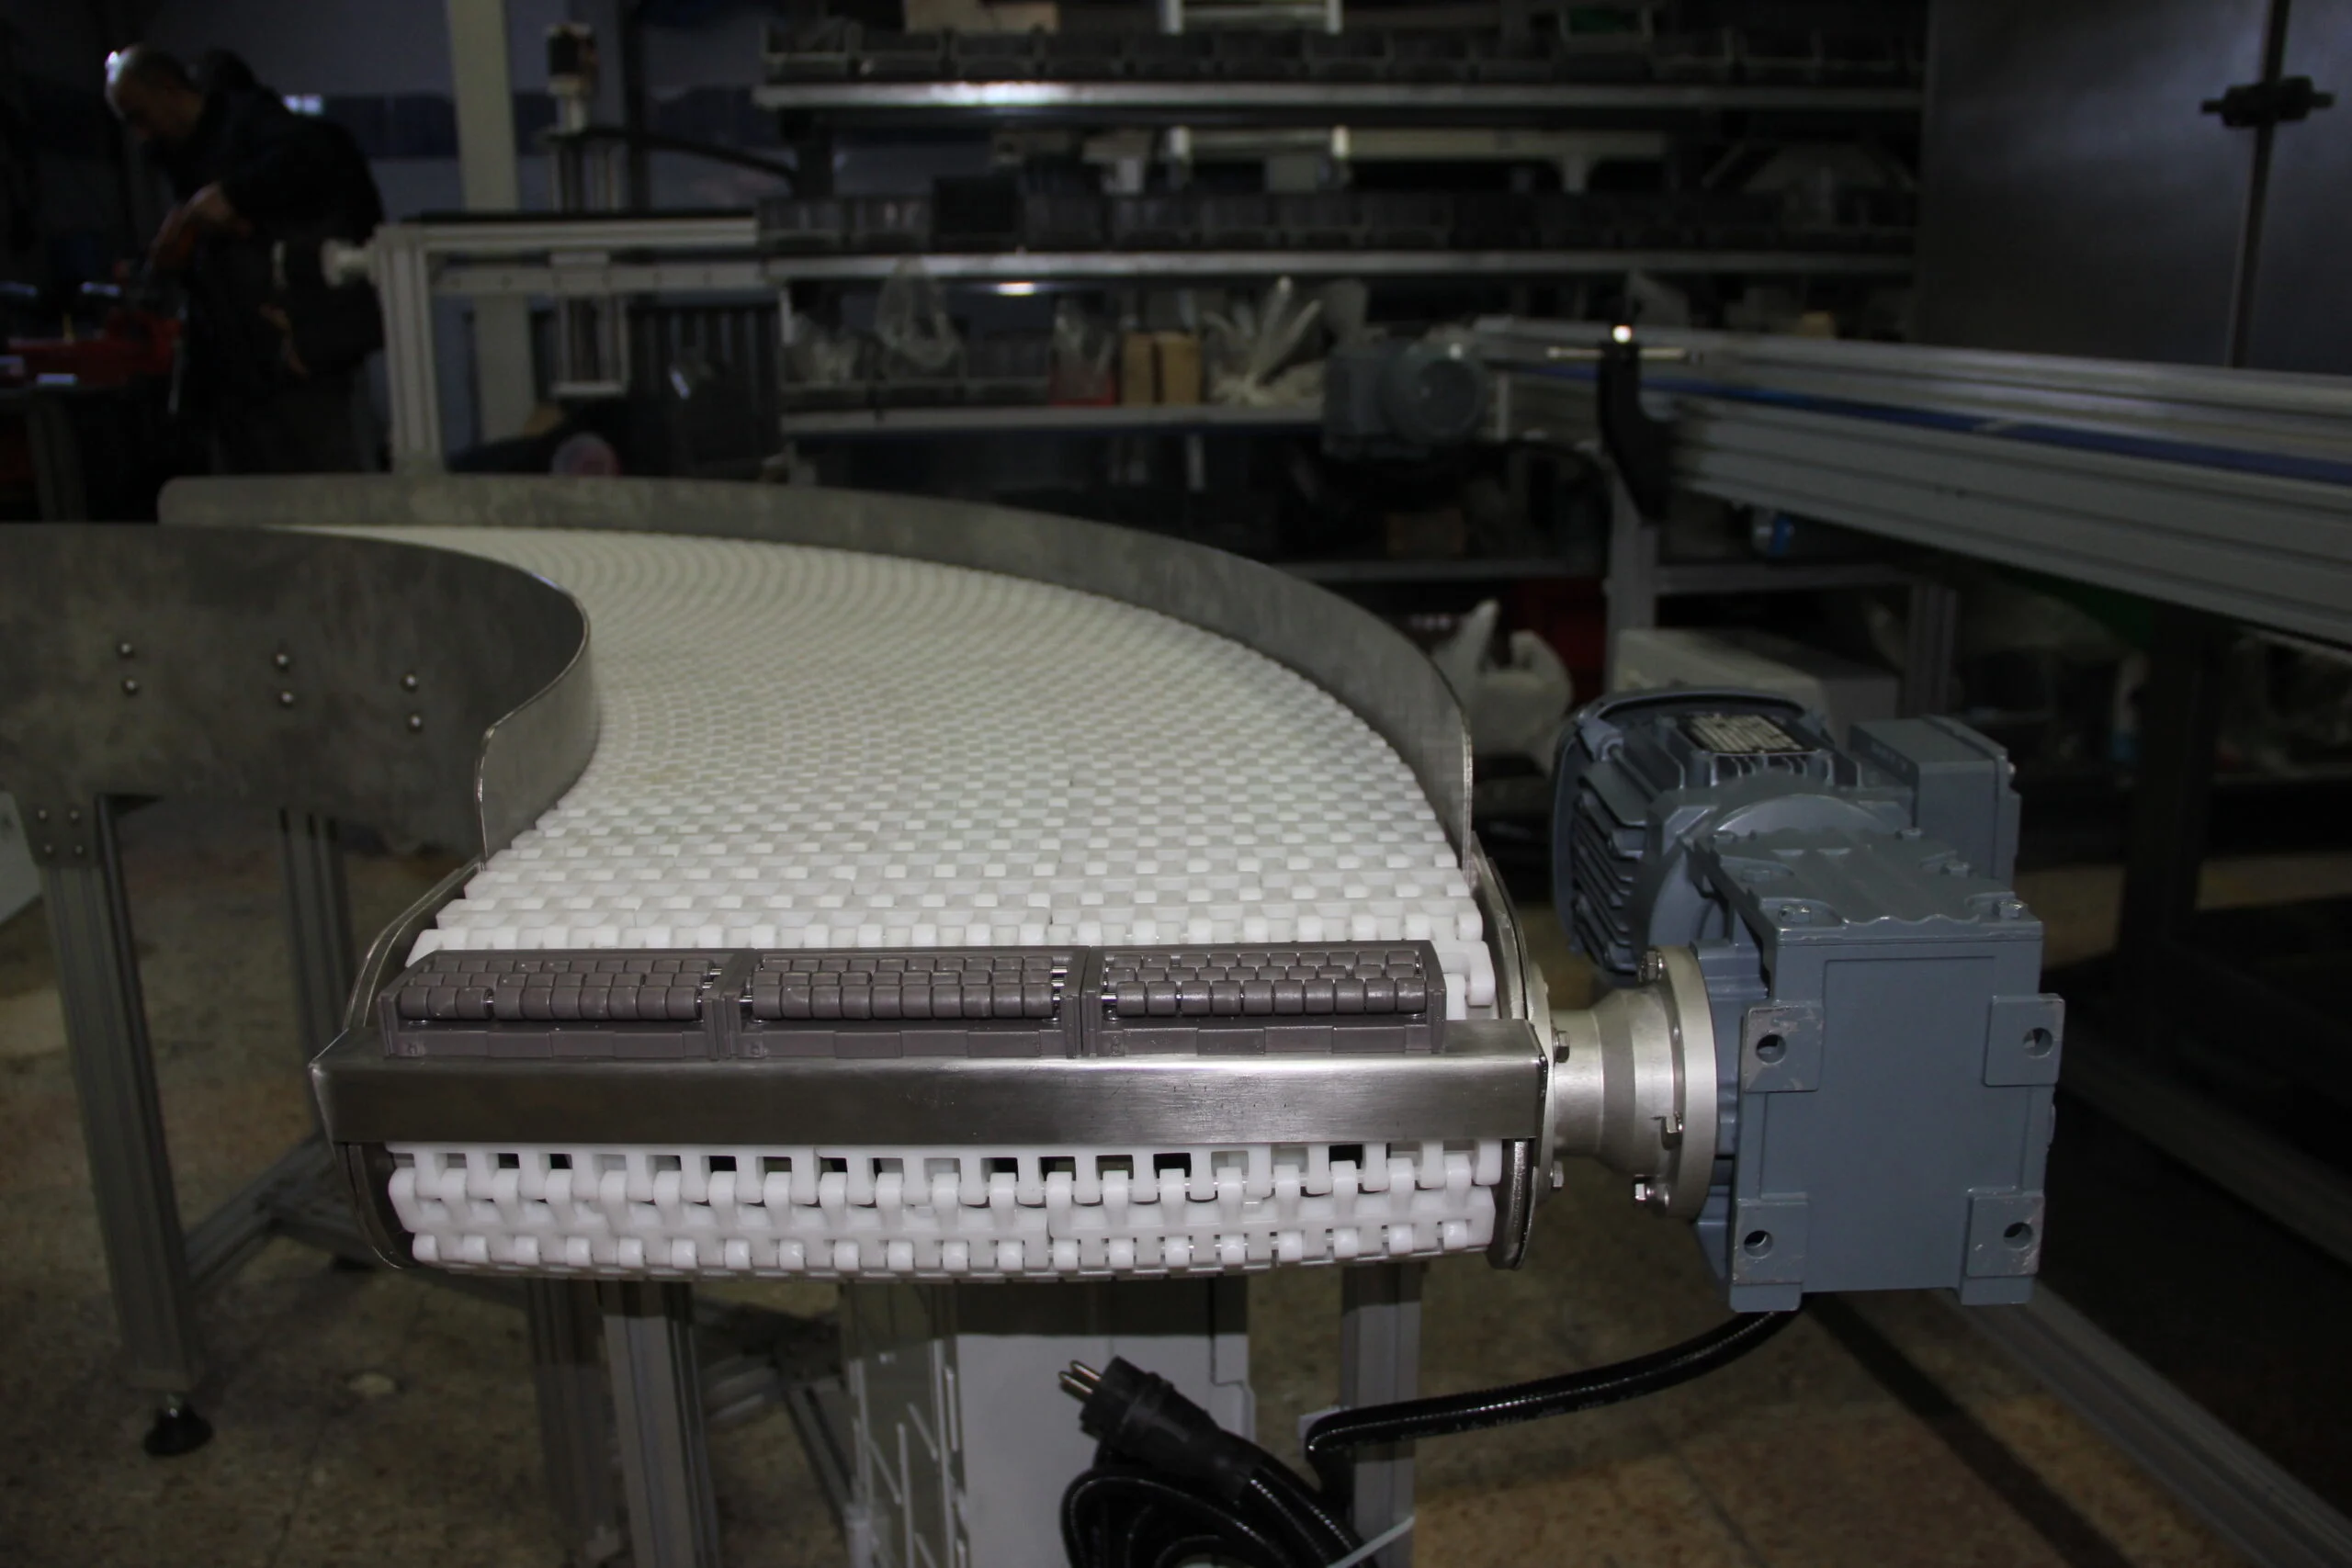
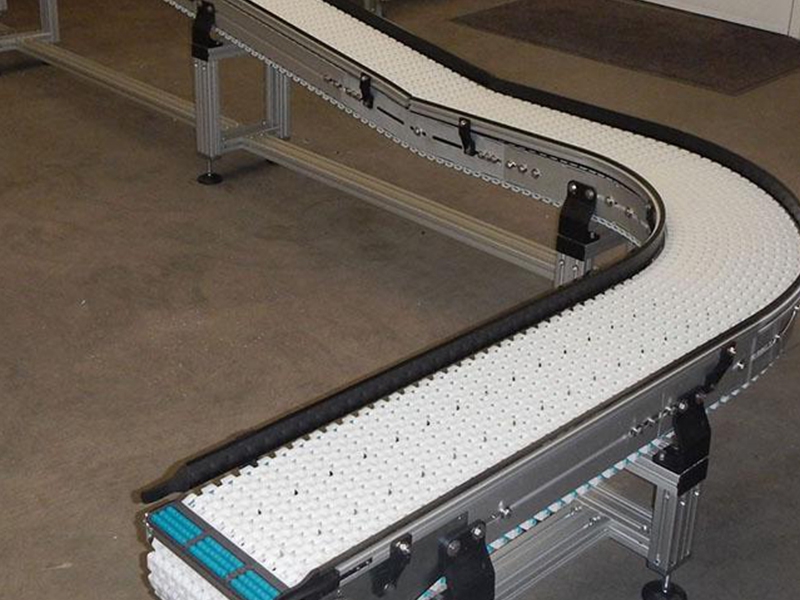
Curved modular belt conveyors are designed to meet the material-handling requirements of different industries through low friction, reduced energy consumption, and easy maintenance.
Activated roller modular belt conveyors are advanced material-handling systems that combine low friction, energy efficiency, and easy maintenance with integrated moving rollers.
Accumulation modular belt conveyors are low-friction, energy-efficient material-handling systems designed to hold and accumulate products in a controlled manner along the production line.
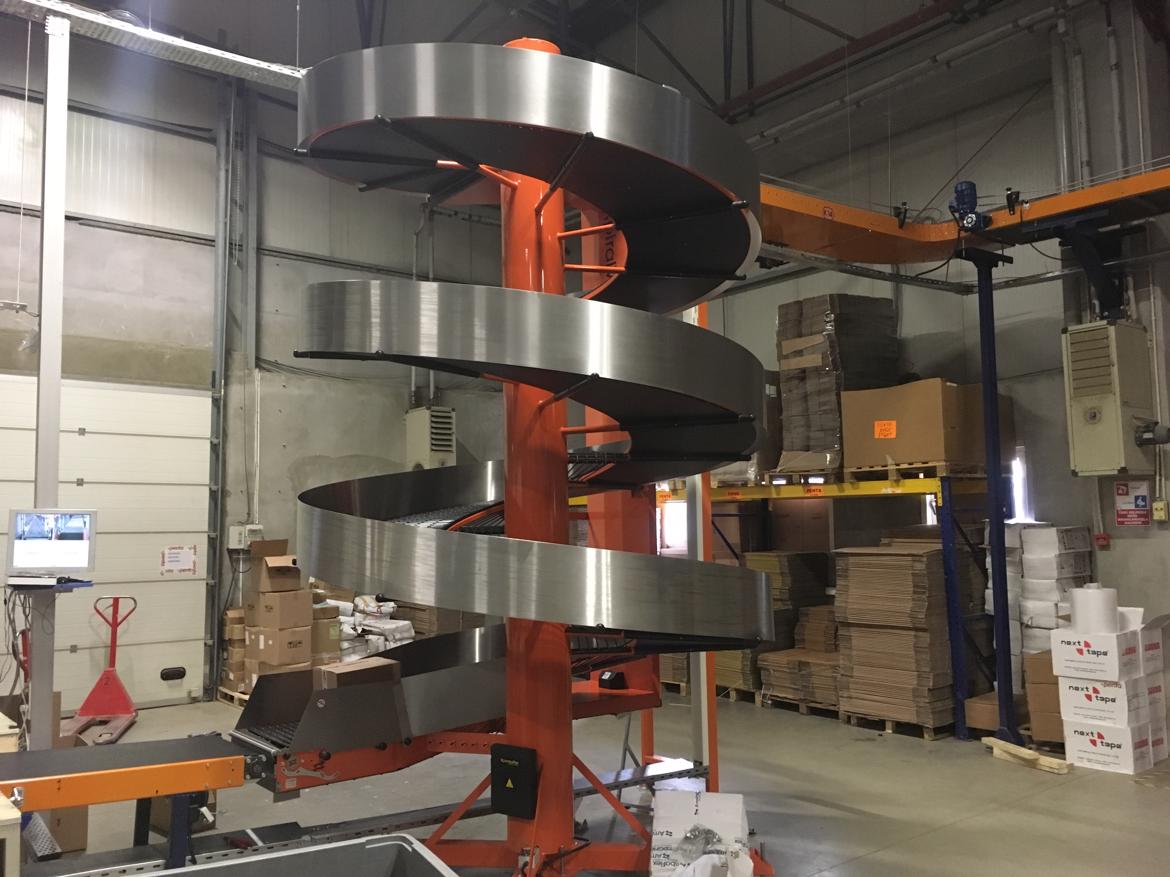
Spiral conveyors are compact and flexible conveyor systems designed to transport products between different levels within limited floor space.
Accumulating roller chain conveyors are commonly used in assembly lines, particularly in the home appliance industry, to transport heavy and large products and accumulate them at designated points in a controlled manner.
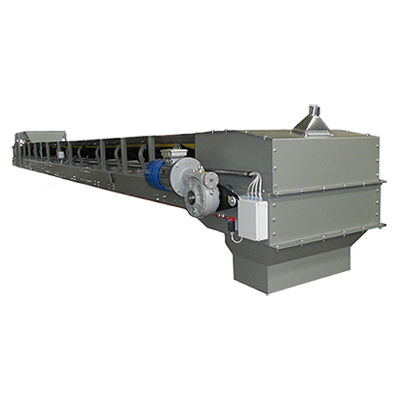
Bulk material conveyors are designed for the safe transportation of granular, powdered, and fine materials, offering high conveying capacity, an enclosed structure, and effective dust containment.
Standard roller conveyors are designed to transport high-tonnage products safely and smoothly.
Timing belt conveyors are designed to transport lightweight and sensitive products smoothly and without vibration or damage.
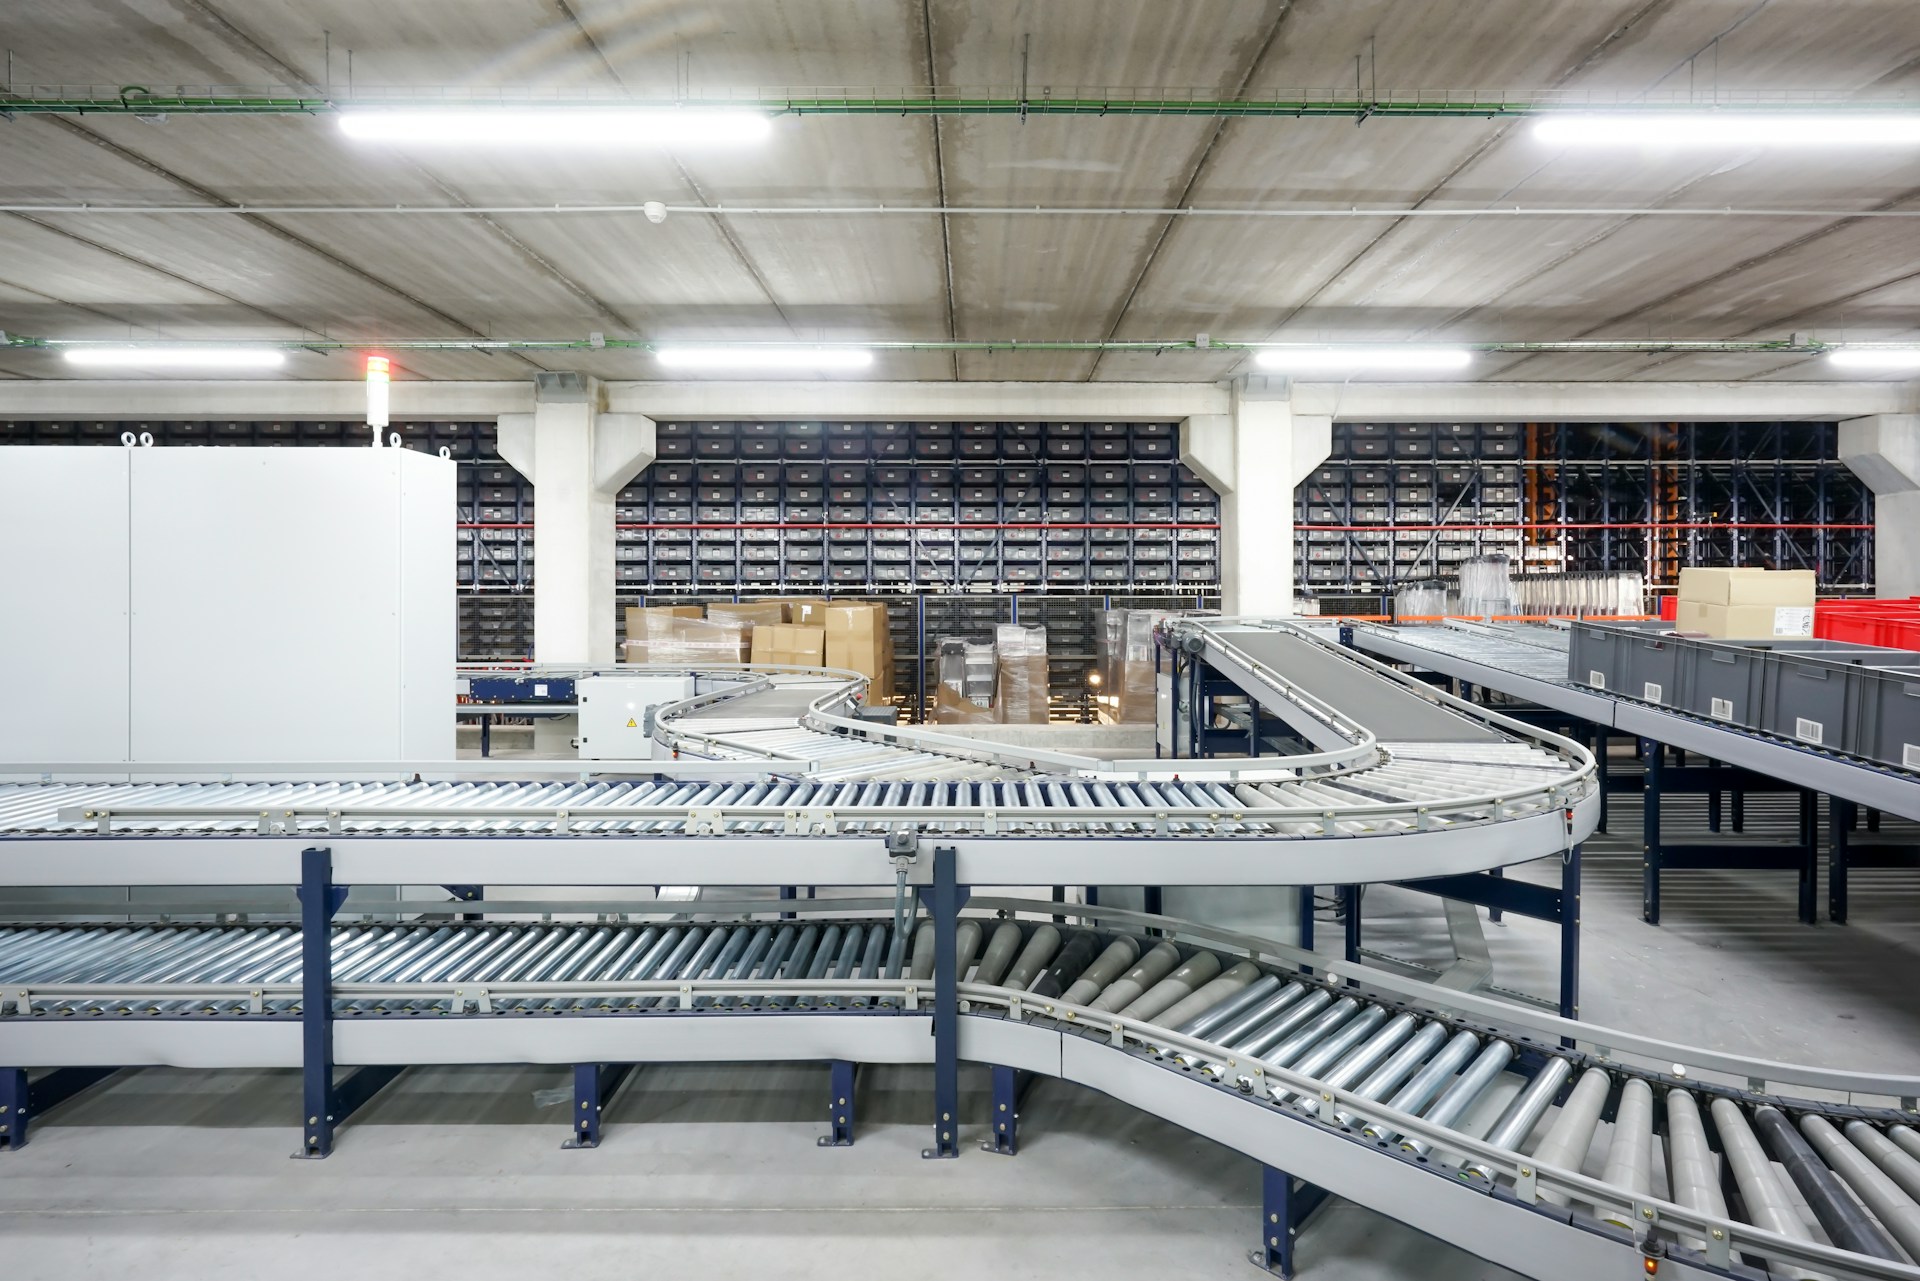
Motor-driven roller conveyors are used to transport products quietly, safely, and efficiently along assembly and production lines.
Gravity roller conveyors are commonly used to transport products and components manually between closely positioned workstations on assembly lines.
Heavy-duty chain conveyors are designed for the safe and reliable transportation of high-tonnage wooden or plastic pallets.
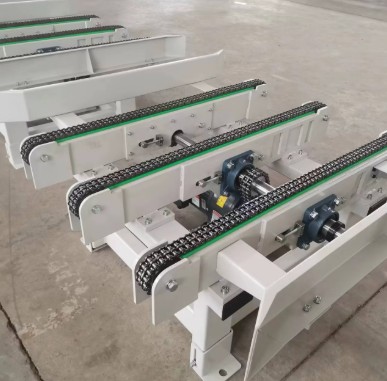
Standard chain conveyors are designed to transport products safely, steadily, and continuously along production and material-handling lines.
Pallet conveyors are chain-driven conveyor systems designed to transport pallets fitted with different types of fixtures.
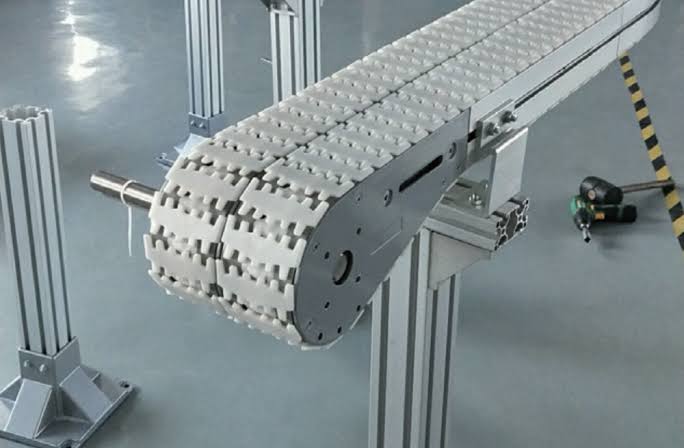
Standard modular belt conveyors are customizable material-handling systems that offer low friction, reduced energy consumption, and easy maintenance for a wide range of industries.
Standard flexible modular conveyors are material-handling systems that offer low friction, reduced energy consumption, lightweight construction, and easy maintenance.
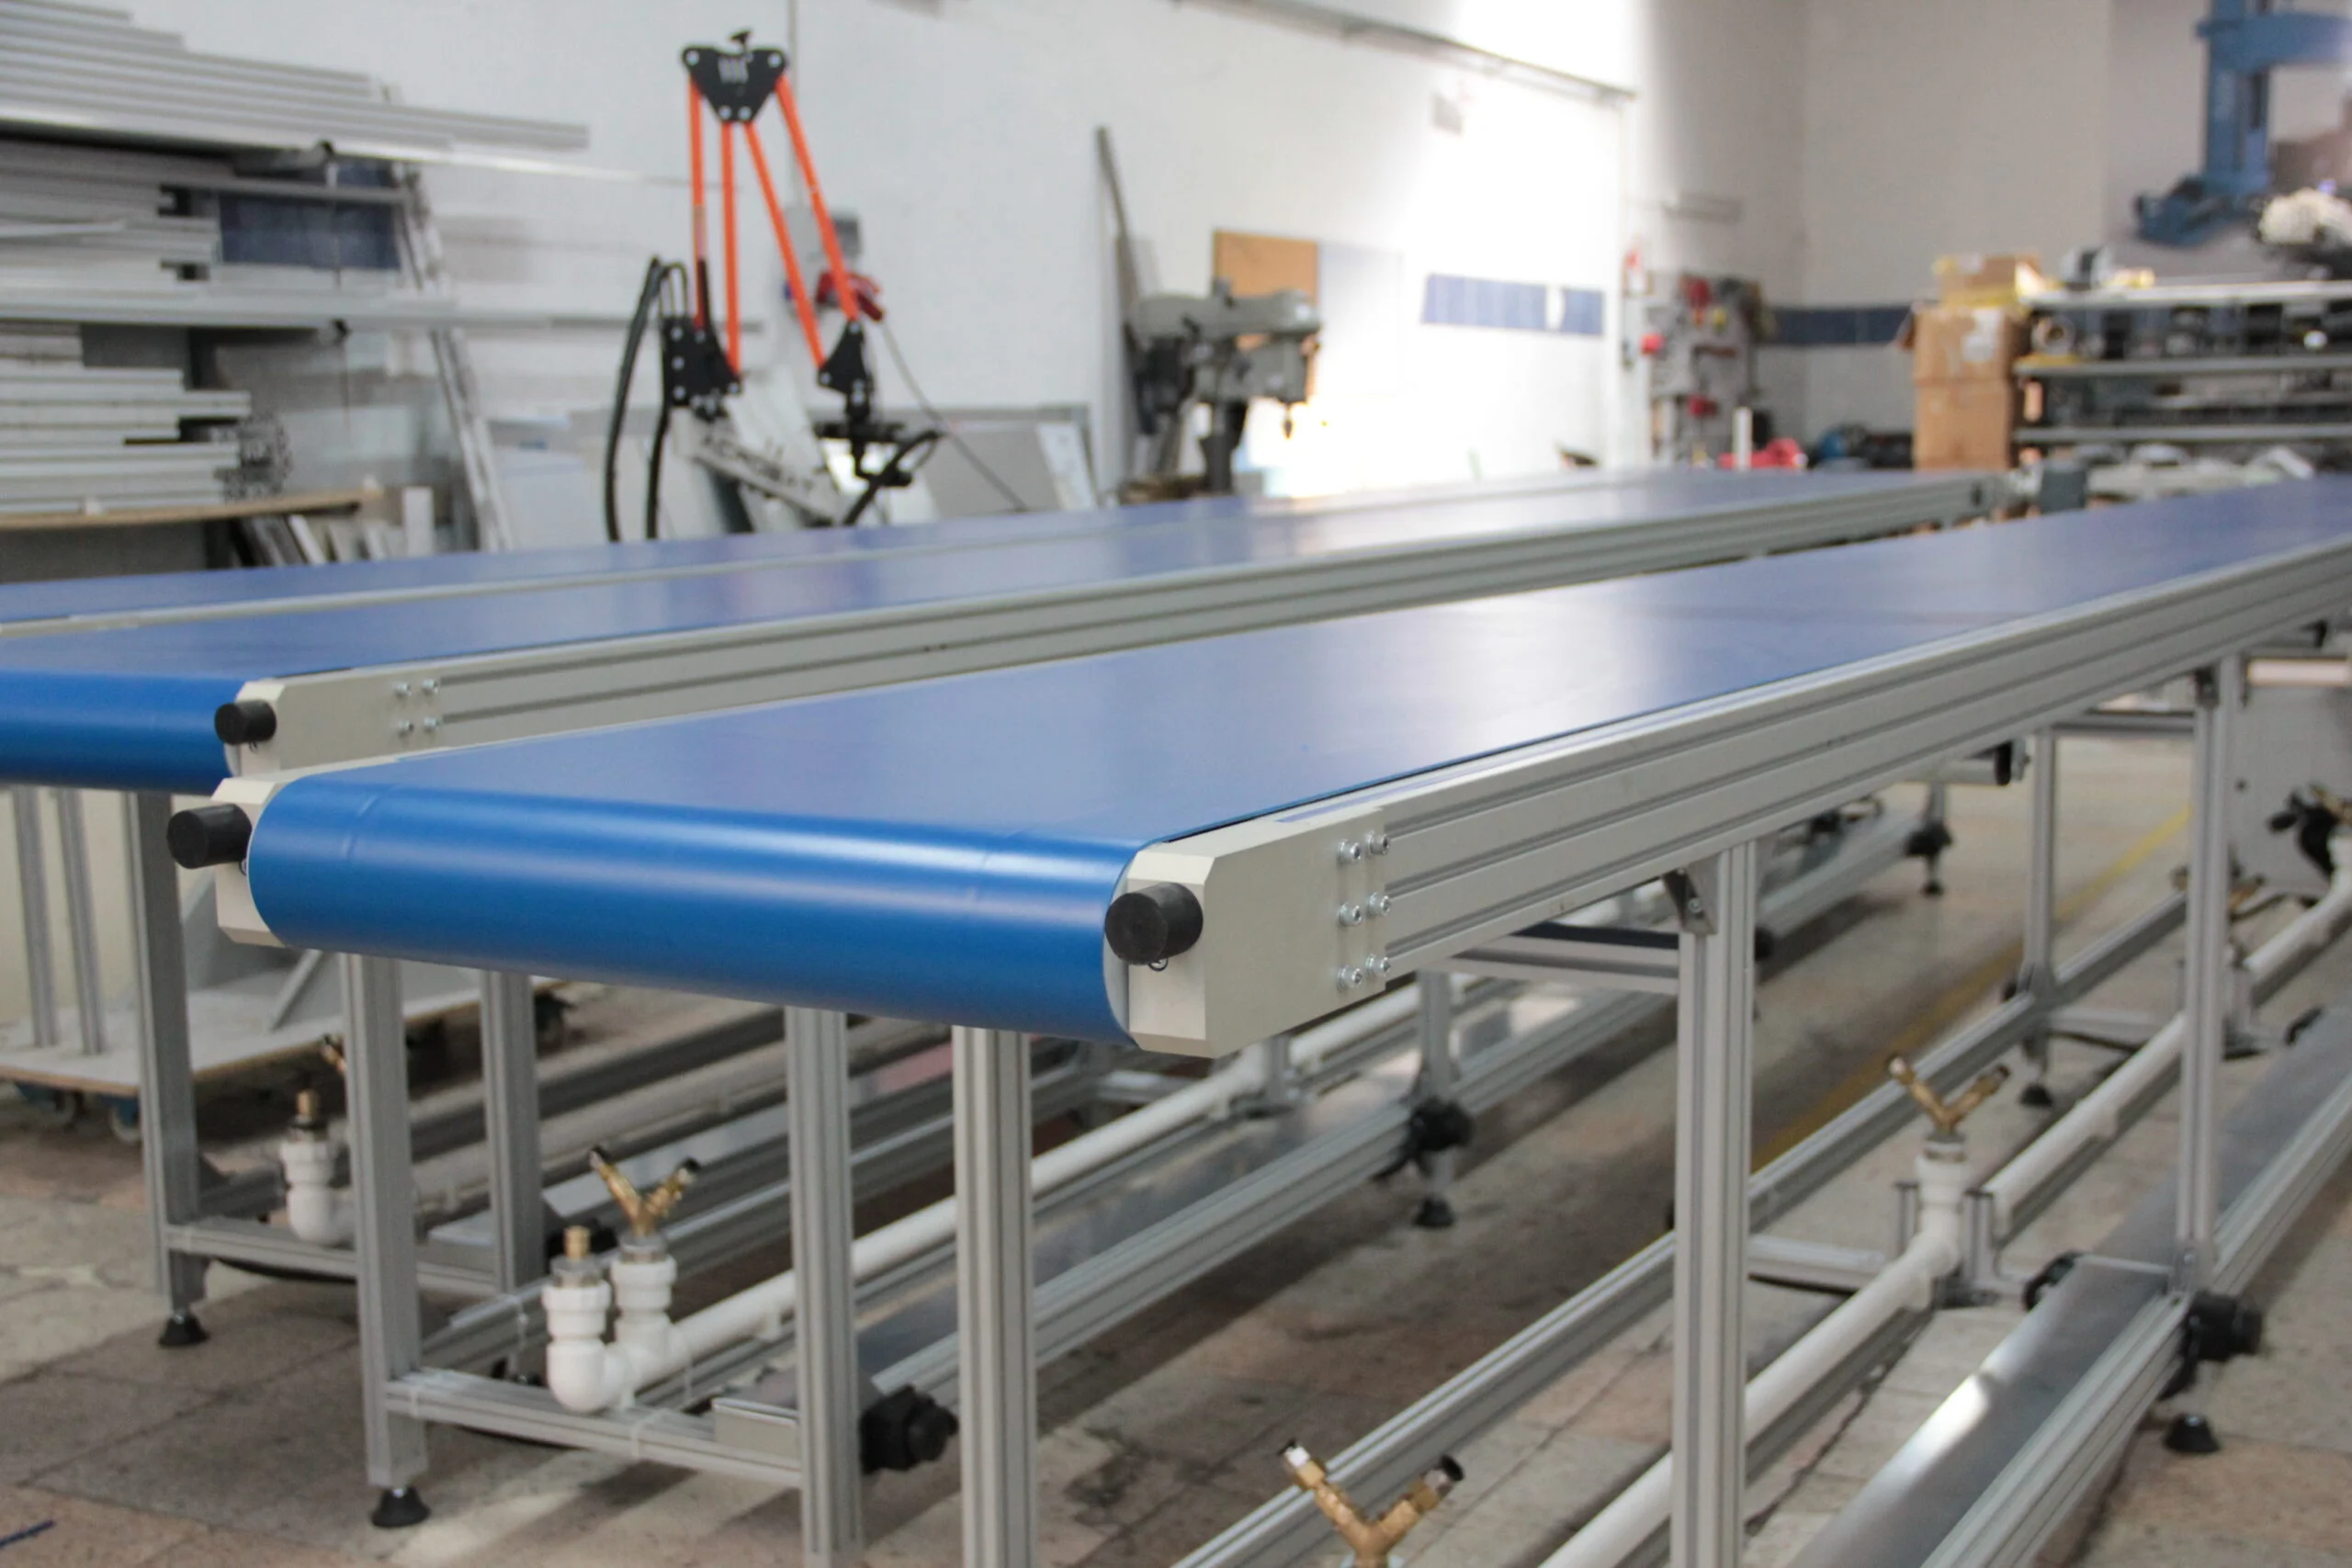
Standard belt conveyors are economical and functional material-handling systems that can be designed with various belt options to meet the requirements of different industries.
Expandable flexible conveyors are versatile material-handling systems that can be extended or retracted through their scissor-type mechanism.
Pneumatic pusher transfer units are designed to divert, transfer, or stop products at designated points along conveyor lines using controlled pneumatic cylinder movement.
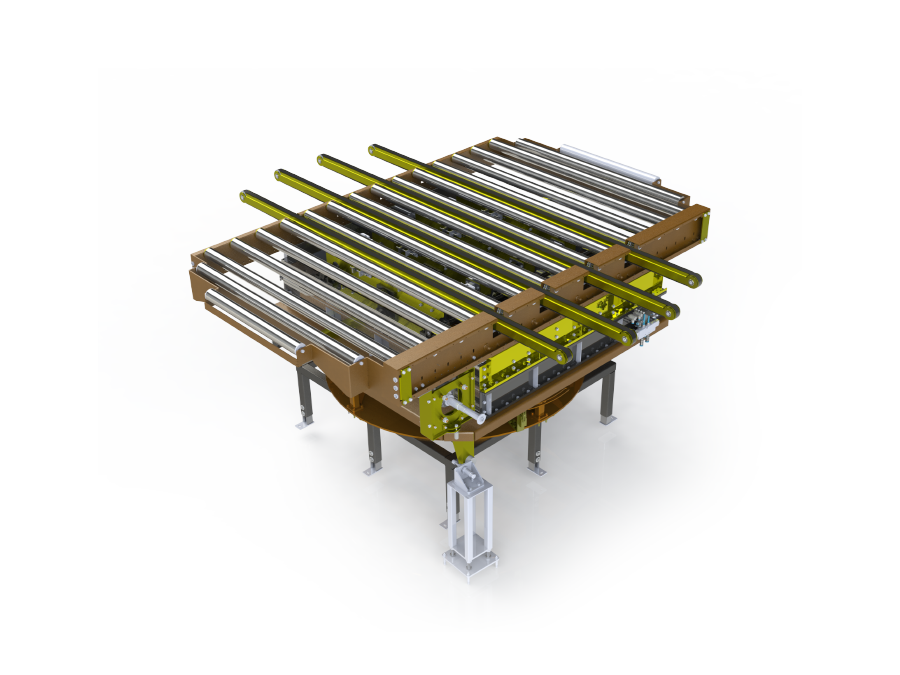
Product turntables are transfer systems integrated into roller chain conveyors to change the orientation of products along production lines.
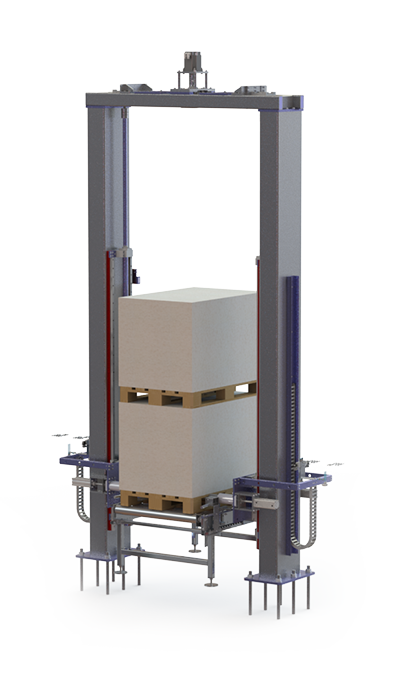
The pallet double-stacking unit is designed to safely and automatically stack pallets moving along the conveyor line.
Pallet magazine systems are designed to store empty pallets efficiently within a compact area and automatically feed them into the material-handling line as required.
Tilting units are designed to rotate products safely and precisely to angles of 30°, 45°, or 90°, while improving operator ergonomics.
Pneumatic centering units are designed to accurately position products moving along a conveyor line before processing, inspection, or transfer operations.
Pneumatic alignment units are used to position, align, stop, or transfer products moving along conveyor lines.
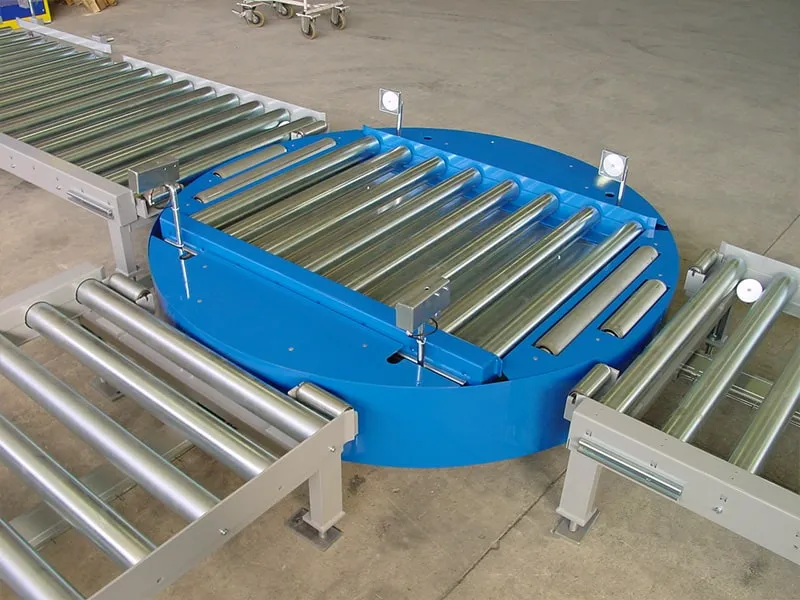
Conveyor turntables are designed to rotate products by 90°, 180°, or 270° and transfer them in different directions along production and material-handling lines.
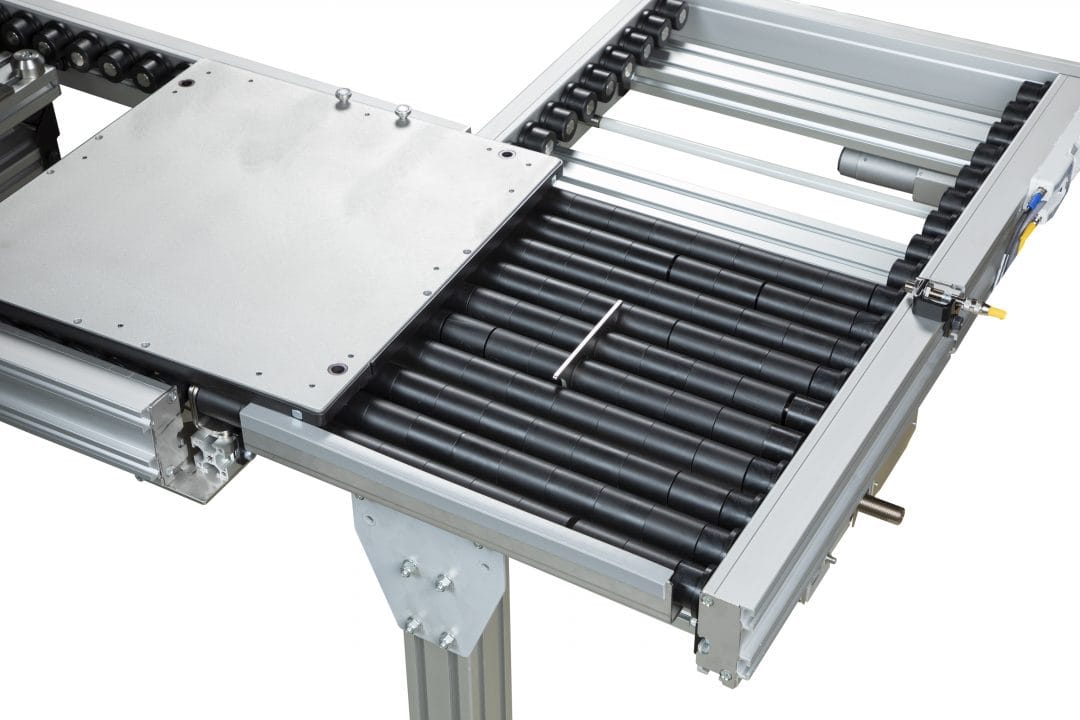
Chain transfer units are designed to transfer wooden or plastic pallets at a 90° angle between conveyor lines. The system operates as an integrated unit within a roller conveyor.
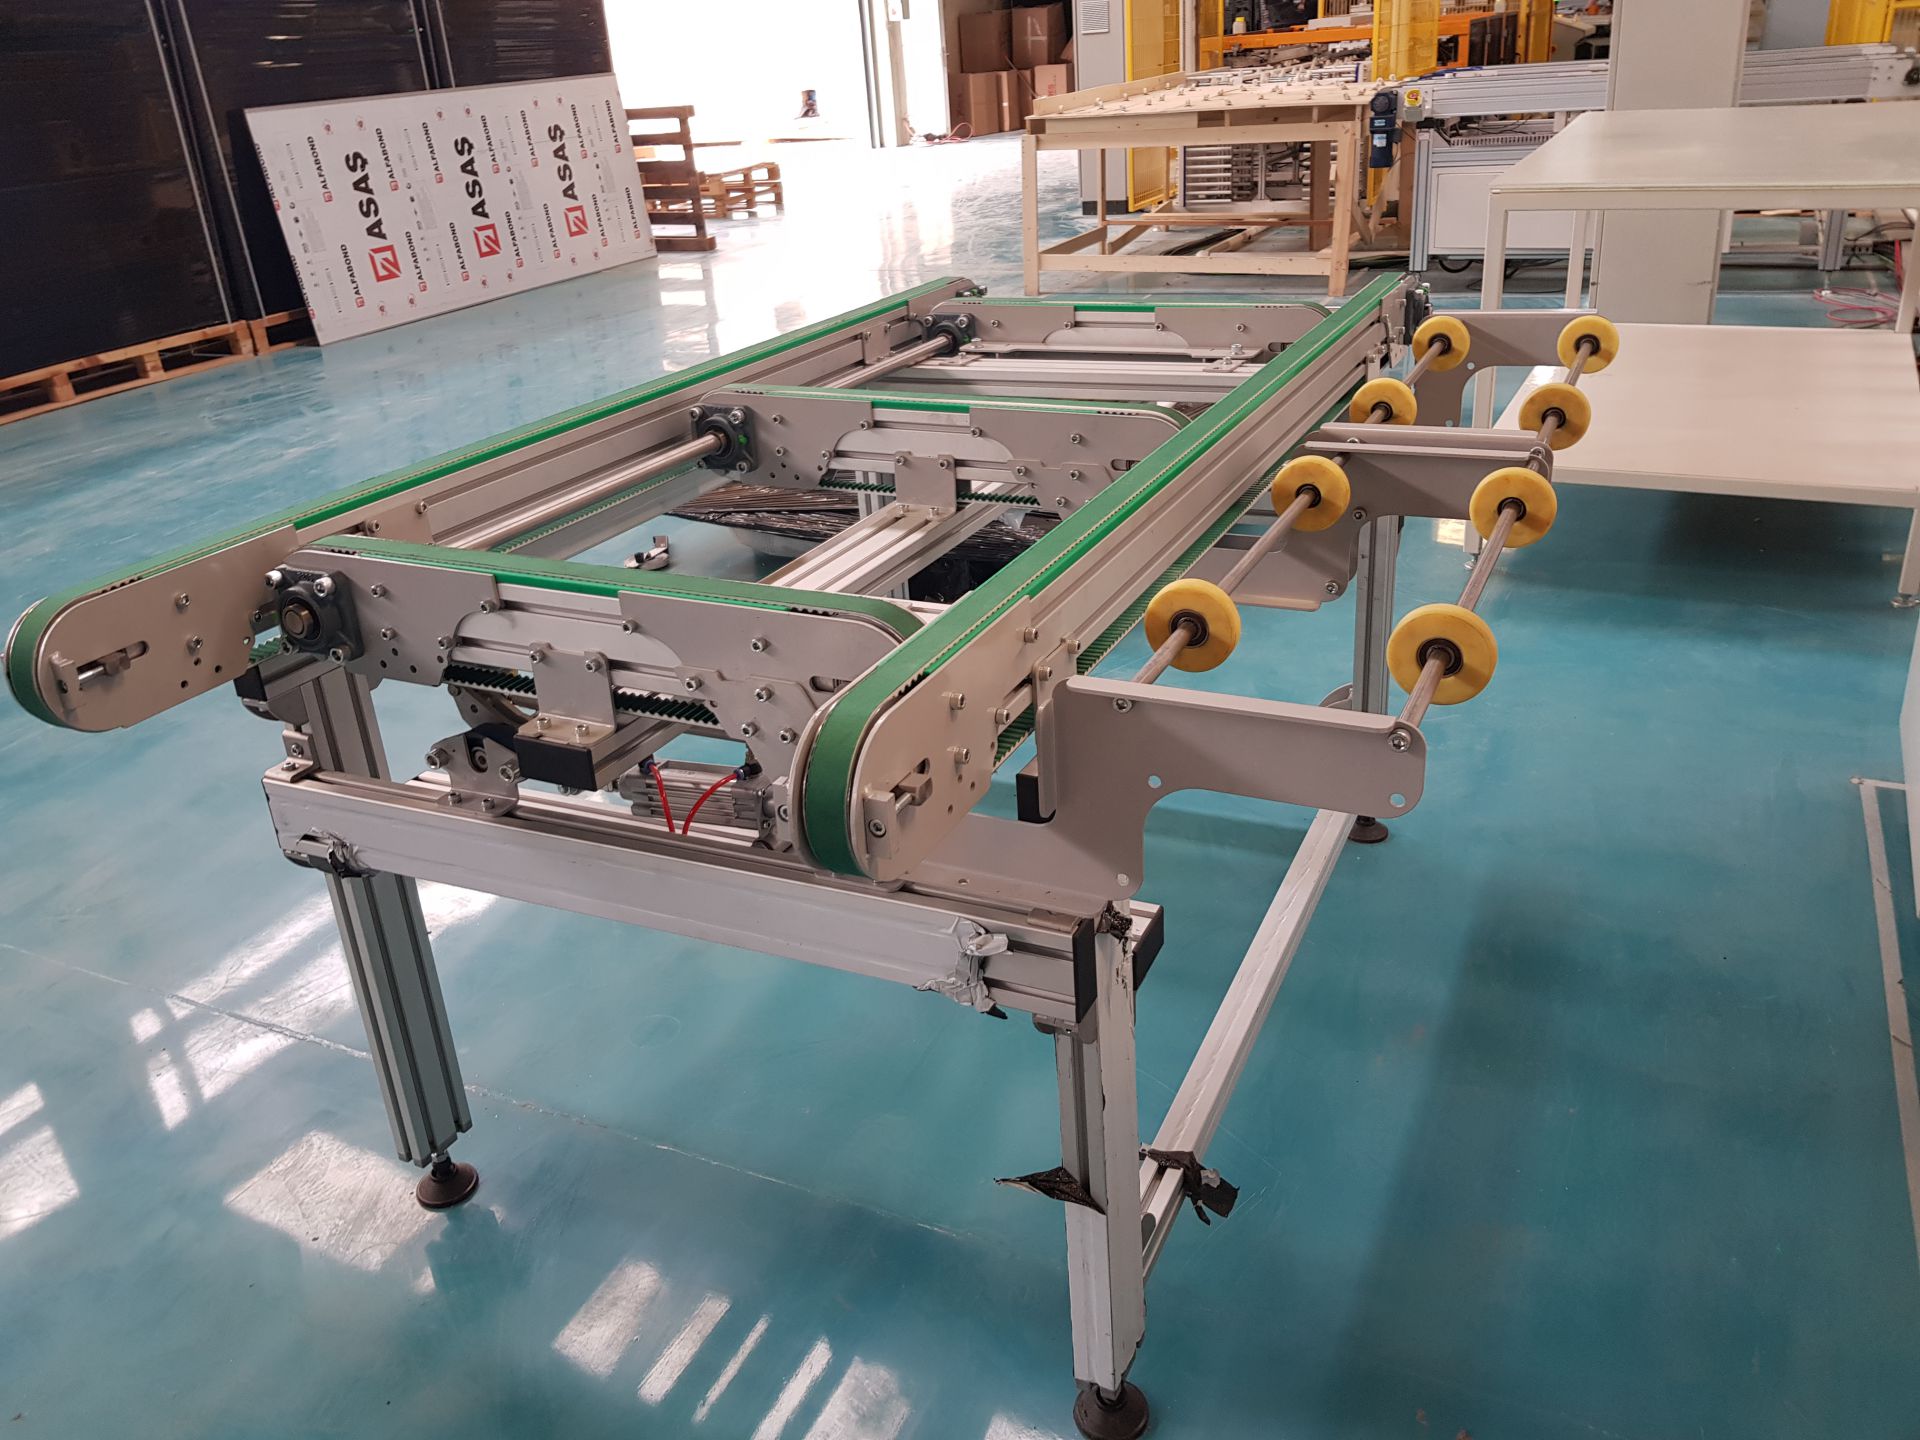
Timing belt transfer units are raised between the conveyor rollers by means of a pneumatic cylinder and connected linkage mechanism, enabling products to be transferred at a 90° angle.
Stop units are used to stop products at designated points on roller conveyors and hold them securely in the required position.
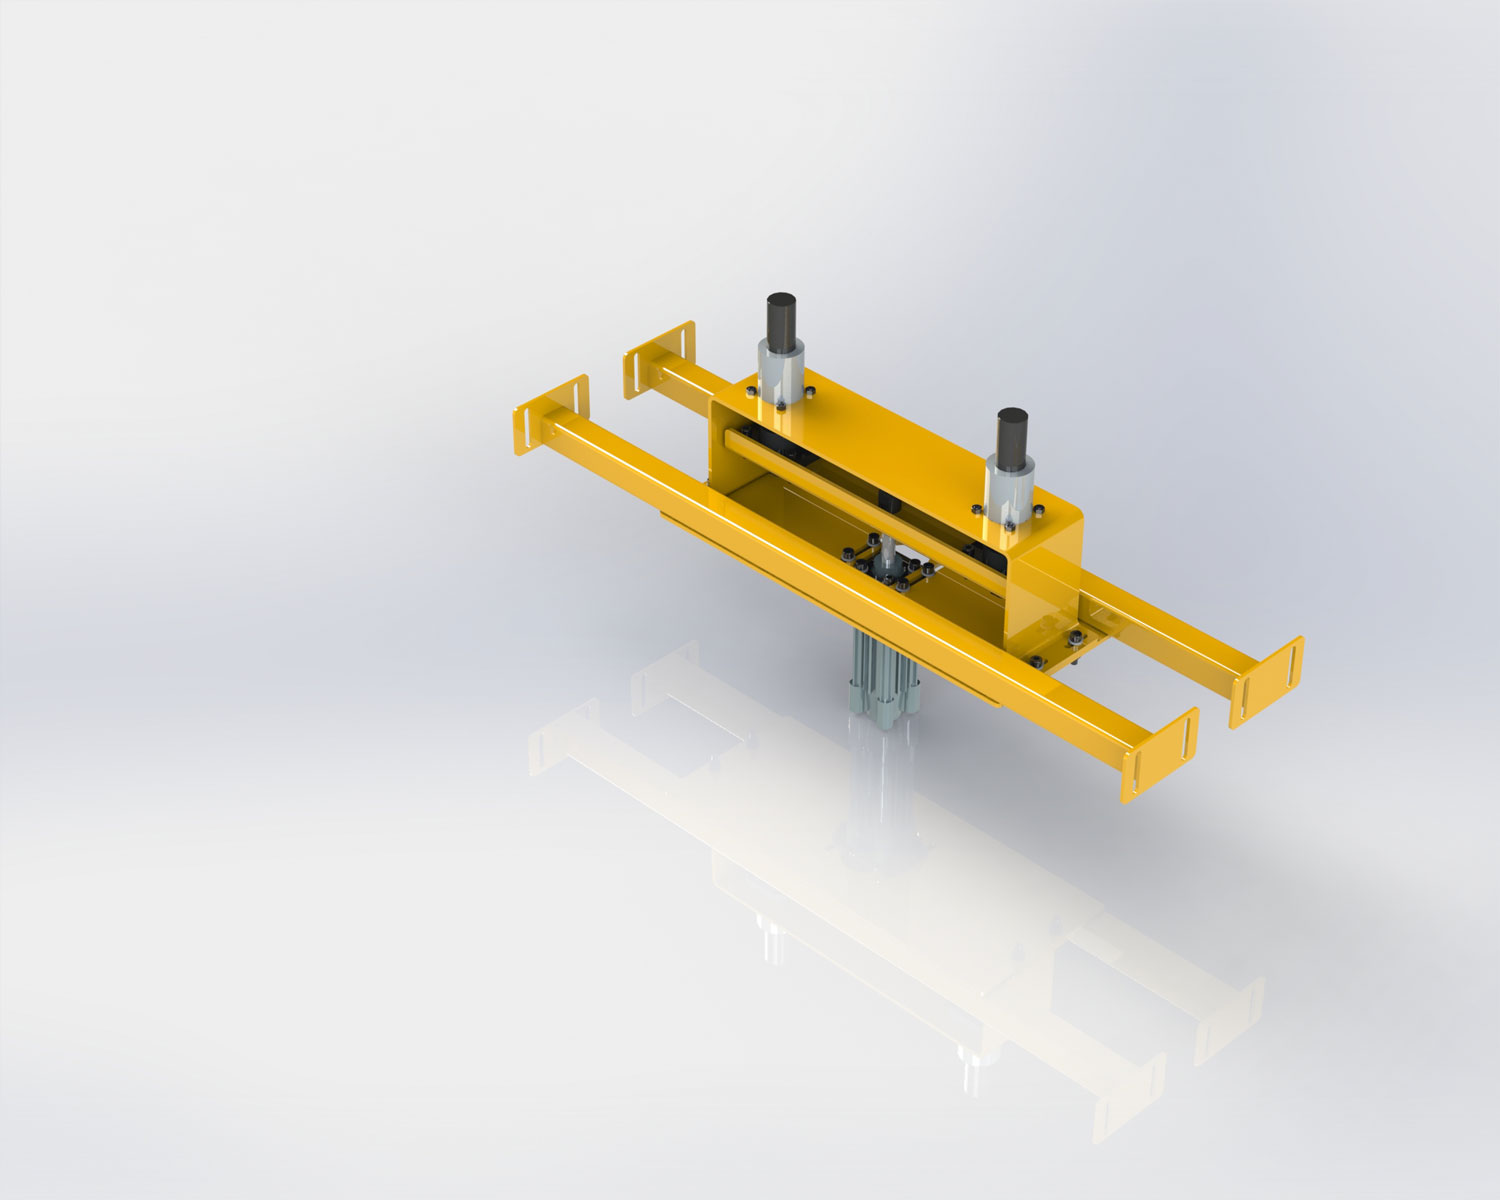
Product rotating units are designed to rotate or invert products in a controlled manner according to the requirements of the production line.
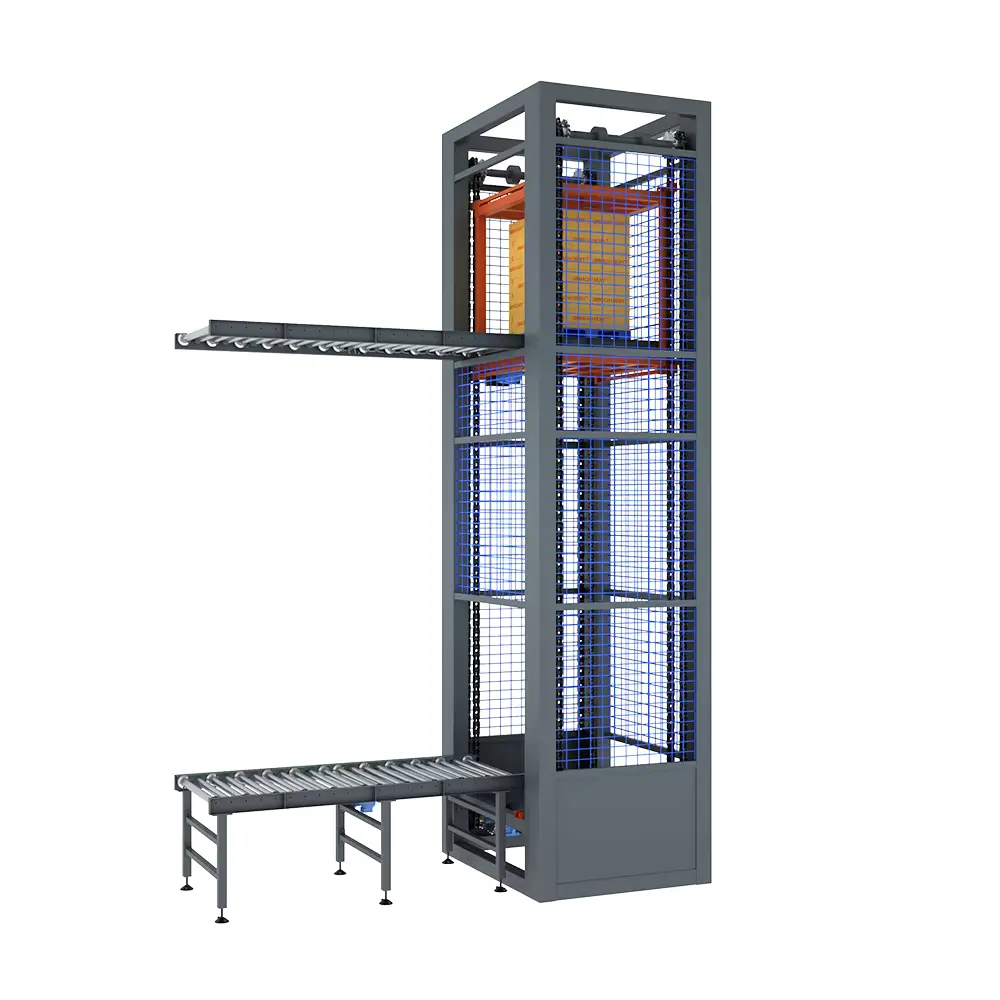
Continuous elevator systems are used to transport products of various sizes and characteristics quickly, safely, and continuously between different levels or elevations.
The Motion Up Elevator is designed for the automatic, fast, and safe transportation of products between different floors and elevation levels.
Pallet lifting units are designed to feed wooden or plastic pallets into conveyor lines easily, safely, and ergonomically.
Motorized lifts are used to raise or lower products and materials safely and precisely between different operating levels.
RGV (Rail Guided Vehicle) shuttle systems are rail-mounted transfer vehicles designed to transport products and loads quickly, safely, and automatically between designated stations.
Pneumatic lifts are air-powered conveying systems used to raise or lower products safely, precisely, and automatically between different operating levels.
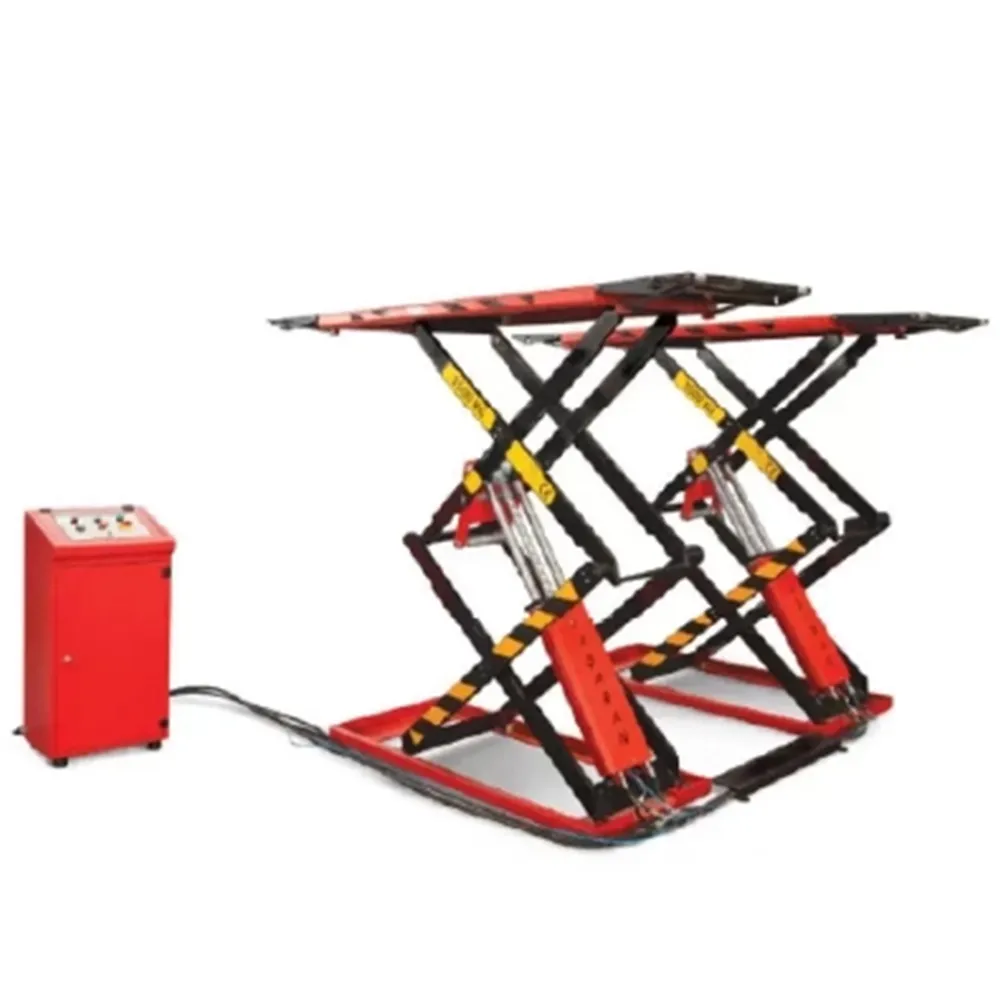
Scissor lifts are designed to transport products automatically, safely, and precisely between different levels along conveyor lines.